
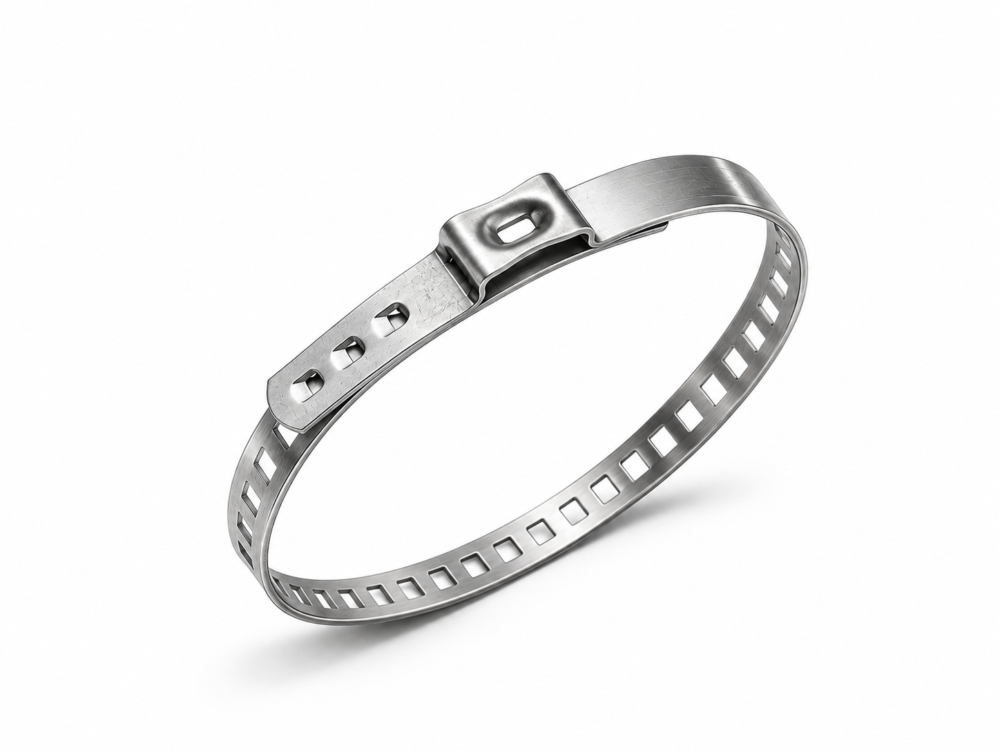
Selecting a different engagement window changes the band overlap and presets the clamp diameter. The load-bearing hook carries band tension during crimping. Where fitted, a locating tab holds the hook in the selected window before closure.
Figure 1 shows outward- and inward-facing hook arrangements. On versions with radial guidance, a guide tab travels in a slot to align the band ends and reduce the internal step at the overlap. Refer to the part drawing for hook orientation and guide design.
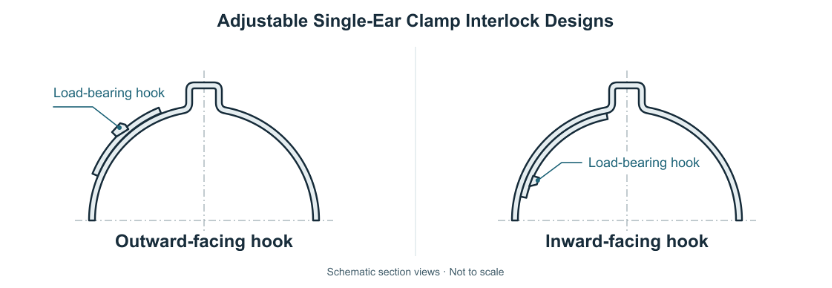
Figure 1 Outward- and Inward-Facing Hook Arrangements
| Series | Band width × thickness (mm) | Ear width (mm) | Series diameter span (mm) |
| TF06A | 7.0 × 0.6 | 10 | 23.6–116.0 |
| TF06B | 9.0 × 0.6 | 10 | 64.0–132.0 |
| TF06C | 7.0 × 0.8 | 10 | 24.5–122.0 |
| TF06D | 9.0 × 0.8 | 10 | 24.5–122.0 |
Seat the hose on the fitting and measure the assembled OD at the clamping location. Check the OD tolerance limits against the diameter range for each part number. Form flat-strip versions into a ring or position preformed versions as specified. Fit axially or, where the design and clearance allow, radially.
Before crimping, select an approved window that brings the band close to the assembly and allows full hook engagement. Check that the locating tab is seated where fitted, the overlap lies flat and the jaws can reach the ear. Include both assembly OD limits in trial builds.
Align matched pincer jaws at the base of the ear and crimp in one stroke at the validated closing force. Closing force is measured in newtons (N). Establish the setting using band dimensions, hose hardness and wall thickness, fitting support and target compression, then validate it on the actual assembly.
Check clamp position, hook engagement, overlap alignment and ear shape. Inspect the hose for abnormal indentation or scoring. Verify sealing or axial pull-off resistance as required by the application. If the assembly falls outside the acceptance limits, follow the approved rework procedure and avoid crimping the same ear again.
Specify the Towin part number, assembly OD limits, band width and thickness, material or finish, flat-strip or preformed delivery, hook orientation and quantity. Include a drawing for special window or guide designs.